About GMP Reaction & Distillation Systems for Bulk Drugs and Active Pharmaceutical Ingredients
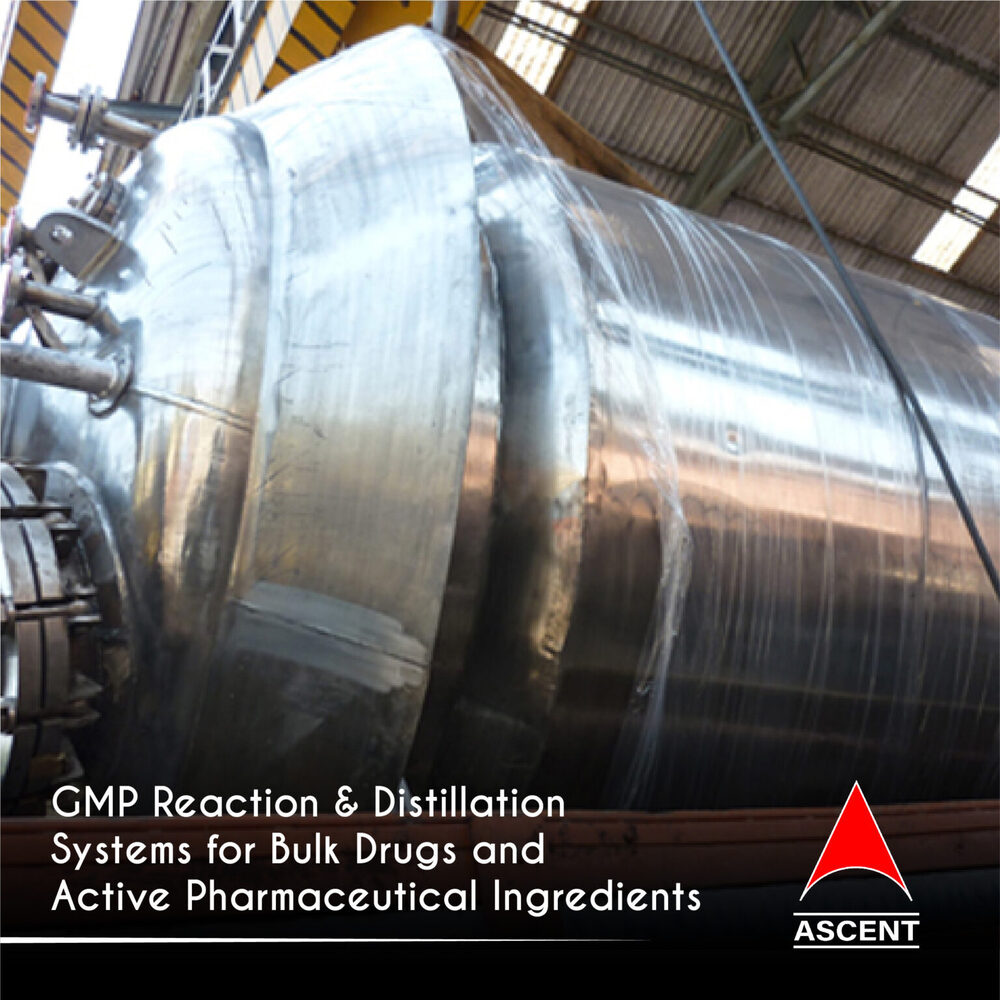
GMP Reaction & Distillation Systems for Bulk Drugs and Active Pharmaceutical Ingredients
Ascent Machineries & Engineering Services manufactures, supplies, and exports advanced GMP Reaction & Distillation Systems designed for the efficient and controlled production of bulk drugs and Active Pharmaceutical Ingredients (APIs). These systems are engineered for hygienic processing, precise temperature and pressure control, and reliable performance in demanding pharmaceutical and chemical manufacturing environments.
Our systems feature reactors with capacities ranging from 50 liters to 10,000 liters and support distillation rates up to 200 liters/hour. They are designed to operate within a temperature range of -50C to 300C and pressure conditions from vacuum up to 10 bar. Reactors and columns are available in SS316L, SS304, and Hastelloy, providing excellent corrosion resistance and long service life.
Key Features:
-
GMP-oriented design for pharmaceutical applications
-
Reactor capacity: 5010,000 liters
-
Distillation rate up to 200 liters/hour
-
Temperature range: -50C to 300C
-
Pressure range: Vacuum to 10 bar
-
SS316L, SS304 and Hastelloy construction options
-
Efficient reaction and distillation performance
-
Customized configurations available
-
Robust and hygienic industrial construction
These systems are suitable for bulk drug manufacturing, API production, pharmaceutical processing, specialty chemicals, and research and production facilities. Ascent Machineries & Engineering Services provides customized reaction and distillation solutions based on process requirements, material compatibility, capacity, and operating conditions, backed by engineering expertise and dependable after-sales support.
High Standards in Design and ComplianceEach system adheres strictly to ASME, DIN, and cGMP guidelines and is engineered for secure handling of high temperatures (up to 300C) and pressures (full vacuum to 6 bar), ensuring regulatory compliance. Expert documentation and validation (DQ, IQ, OQ, PQ) support global regulatory acceptance, making them suitable for US FDA, WHO, and EU-regulated environments.
Versatile Operation and ControlOur solutions feature advanced process control with options for SCADA, HMI, PLC, and DCS-based automation. Whether semi-automatic or fully automatic, clients benefit from electronic batch record-keeping. Flexible utilities, agitation systems, and various safety enhancements guarantee reliable and efficient operation for a range of processing needs.
Customizable for Diverse ApplicationsWith customizable capacities, material selections, and configuration layouts, the systems are ideal for diverse production scales, from pilot to large batches. Accessories like condensers, phase separators, and vacuum pumps can be integrated as required. Material selection and surface finishes support robust, hygienic performance and easy maintenance.
FAQ's of GMP Reaction & Distillation Systems for Bulk Drugs and Active Pharmaceutical Ingredients:
Q: How are GMP Reaction & Distillation Systems customized for different pharmaceutical processes?
A: Our systems are tailored to client specifications regarding capacity (from 50L to 30,000L), materials (SS316, SS304, or Hastelloy), pressure and temperature ratings, agitation type, and control systems. This ensures optimal performance for reactions, purifications, solvent recoveries, and other API or bulk drug manufacturing steps.
Q: What documentation and quality assurances are provided with these systems?
A: We provide a full suite of DQ, IQ, OQ, and PQ documentation in alignment with cGMP, US FDA, WHO, and EU guidelines. Every unit is built under a GMP-certified quality system, ensuring consistency, traceability, and regulatory approval for pharmaceutical use.
Q: When should a manufacturer consider an automatic or semi-automatic system variant?
A: The choice between automatic or semi-automatic variants depends on production volume, process complexity, and desired level of operator intervention. Automatic systems with PLC/DCS and HMI integration are ideal for high-volume and complex operations needing minimal manual input and advanced data management.
Q: Where can these reaction and distillation units be installed?
A: Units are designed for pharmaceutical production facilities involved in API, intermediate manufacturing, or solvent recovery. With customizable dimensions and capacity, installation is feasible in both new setups and upgrades of existing GMP-compliant facilities.
Q: What is the process for installation and commissioning?
A: Our service includes on-site installation and commissioning, ensuring that all connections, validation processes, and operational checks meet GMP and project requirements. Training and technical support are also provided to enable smooth transition to production.
Q: How are cleaning and maintenance facilitated in these systems?
A: The systems feature manways, cleaning ports, and are CIP (clean-in-place) and SIP (sterilization-in-place) capable. This design ensures efficient cleaning, maintenance access, and long-term hygienic operation with minimal downtime.
Q: What are the primary benefits of using your GMP Reaction & Distillation Systems?
A: Users benefit from high process reliability, precise control, regulatory compliance, and flexible design. The systems support safe, efficient, and reproducible manufacturing of APIs and related products, bolstered by robust documentation, safety features, and easy-to-maintain hygienic design.





 Send Inquiry


 Send Inquiry
 Send Inquiry
 Send SMS
 Call Me Free


 English
 Spanish
 French
 German
 Italian
 Chinese (Simplified)
 Japanese
 Korean
 Arabic
 Portuguese
